A small Australian manufacturer receives a batch of machined housings. Some assemble cleanly; others need rework. A supplier offers a 3D scanner that produces detailed models and colourful deviation maps. Should the business buy it?
The useful question is not whether the scan looks impressive. It is whether the measurement can support a specific acceptance decision, reliably, on the parts the business actually makes. This practical guide draws on established NIST measurement research. It is not a new product announcement or an Australian compliance standard.
Start with the decision, not the scanner
Choose one recurring problem: checking a curved external profile, documenting a casting, or comparing a manufactured surface with an approved CAD model. Record the relevant drawing revision, features, tolerances and who is authorised to accept or reject the part.
Some jobs do not need a full surface scan. A suitable gauge or coordinate measuring machine may be more appropriate for a critical bore or tight dimensional requirement. If the scanner cannot see a feature, an attractive exterior model does not make that feature inspected.
Understand what structured light measures
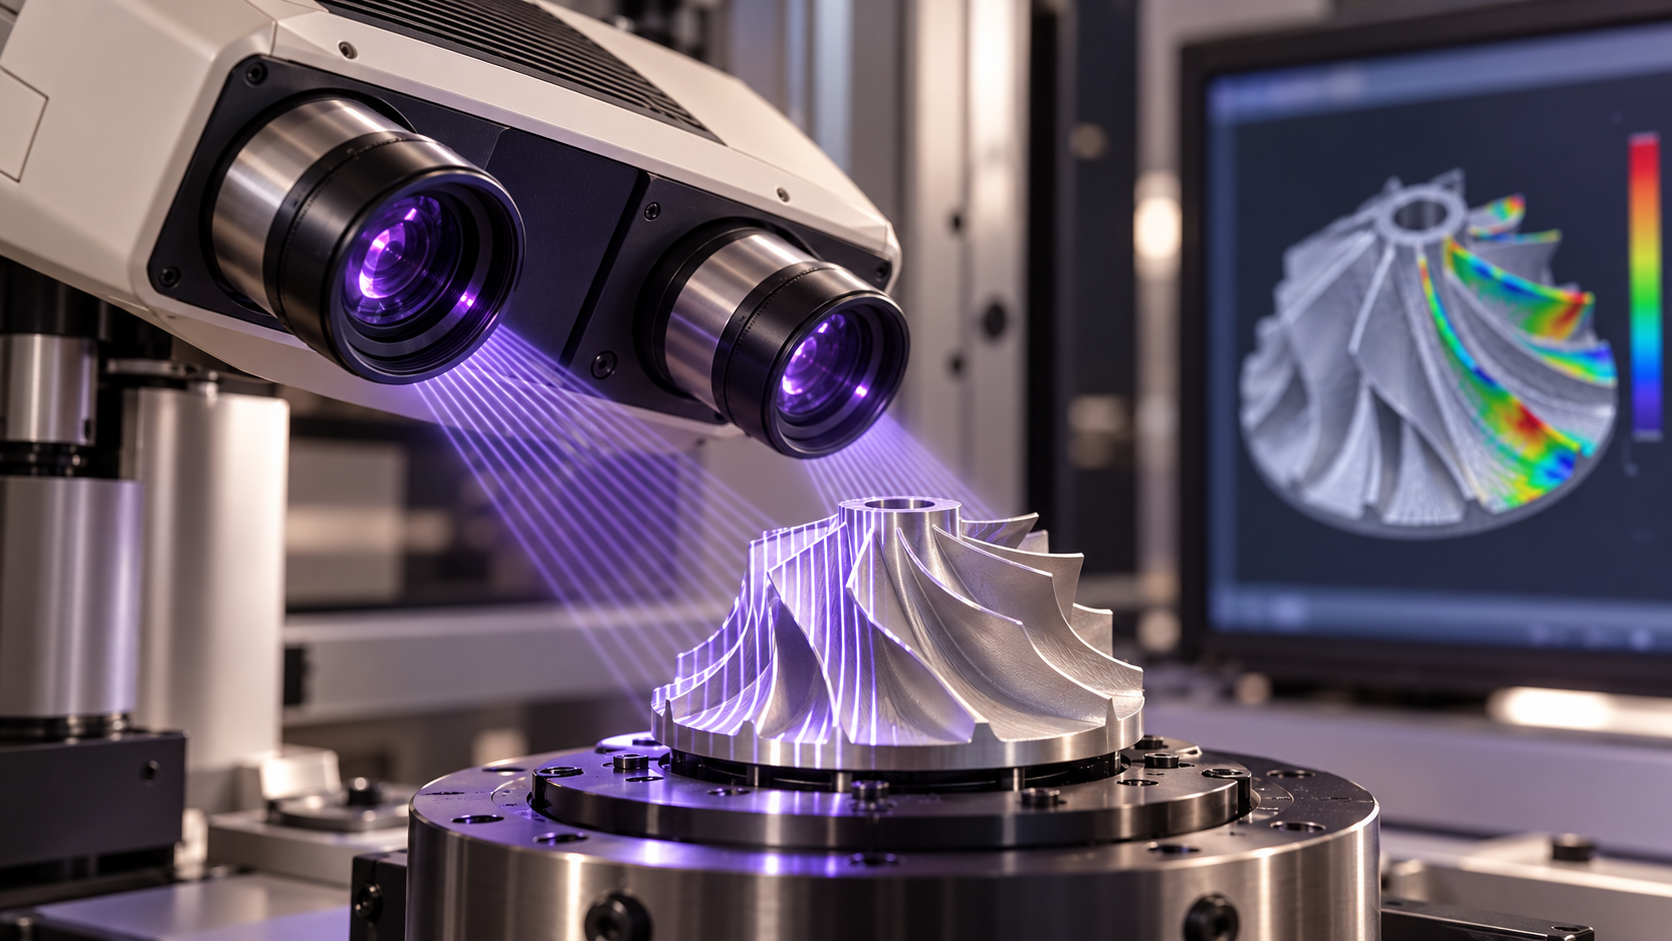
A structured-light scanner projects patterns onto an object. Cameras observe the patterns, and the system calculates surface coordinates using triangulation. Software combines the captured data into a model for inspection or other uses.
NIST’s research identifies several sources of error, including scanner construction, the target surface, environmental conditions, operating settings and data processing. Its findings are a useful warning against treating a headline accuracy figure as a guarantee for every part. The research is established technical work, not evidence about the performance of a particular current product.
Point density and measurement accuracy answer different questions. A model with many points can still contain systematic errors. Smooth rendering, a small file-to-model distance or an attractive colour map is not, by itself, proof of a trustworthy acceptance decision.
Make the supplier trial your awkward parts
Use representative production samples, not only the supplier’s demonstration object. Include the finish, size, recesses and variation that create problems in your process. NIST discusses challenges with deep, dark and shiny features, as well as changes in performance across the measurement volume.
For example, a cast housing may have an easily scanned outside surface but a deep internal pocket that remains incomplete. Surface treatment might improve a scan, but ask whether preparation is permitted for your product and how it affects dimensions, cleanliness and handling time. Do not quietly fill missing geometry in software and treat it as measured data.
Run a comparison that can fail
Agree the pilot’s pass conditions before viewing the results. A sensible trial could include the following activities:
- Repeat scans after removing and repositioning the part, rather than simply reprocessing the same capture.
- Have another trained operator repeat the process using documented settings.
- Compare important dimensions with a suitable independent measurement method, selected with a metrology specialist where needed.
- Include known acceptable, unacceptable and borderline samples where these are available.
- Keep records of preparation, capture, alignment, review and report-generation time.
Repeatability matters, but repeating the same wrong answer is not enough. Assess measurement uncertainty and suitability for the required tolerance with qualified advice. Where the result cannot confidently support acceptance, retain another inspection method.
Control the software as carefully as the optics
Agree how the scanned part is aligned with its reference model. A best-fit alignment can be useful for investigating shape, but may not represent the drawing’s required datum-based inspection. Ask the supplier to explain the difference using your part.
Save the approved model revision, raw capture where practical, alignment method, filtering settings, software version and inspection report. Keep measured areas distinguishable from interpolated or missing areas. Give each result a clear link to the relevant job or batch.
For a small team, this is also a workflow problem. Decide who reviews exceptions, where evidence is stored and how results reach the production or inventory system. Avoid automatically releasing stock from a colour map until the measurement process and decision rules have been validated.
Buy capacity only after proving the job
Compare purchasing with hiring a scanner, using a specialist inspection service, or improving the existing gauge process. Include software licences, training, calibration or verification arrangements, fixtures, surface preparation and support in the business case. Do not assume the fastest capture produces the fastest completed inspection.
A useful next step is to send a supplier one drawing and a small set of representative parts, then request a documented demonstration of the actual accept-or-reject decision. If that cannot be demonstrated, a larger equipment order will not resolve the uncertainty.
Xpansion Technologies can help plan how inspection records connect to business software and production workflows. Scanner selection, measurement uncertainty and acceptance methods should be assessed with an appropriately qualified metrology provider.
Sources
Leave a comment